How to Choose a Thermal Interface Material Supplier
Eight checks that separate a real thermal interface material supplier from a reseller: certificate scope, test conditions, Cpk, traceability and lead time.
A thermal interface material supplier is qualified on eight things: certificate scope, test conditions, process capability, lot traceability, compliance documents, conversion capability, capacity and lead time, and commercial terms. Three of those are visible in a quotation. The other five decide whether the material is still the same material in month nine of production.
Most supplier reviews stall at the same place. Three quotes arrive, every datasheet says something in the 3 W/m·K range, the prices differ by twenty percent, and nobody in the room can explain why the more expensive option is the safer one. So the decision gets made on price and the risk gets carried until a build fails.
The eight checks below are the ones that close that gap. Each one has an owner, a document or answer that satisfies it, and a signal that means stop. Worked through in order, they take an OEM buyer from first contact to a defensible supplier decision inside a month — without a test lab of your own.
This guide is written for the buying side: sourcing engineers, quality engineers and thermal designers running a first or second source qualification for a program that will go to volume. If you are still choosing between a thermal pad and a gap filler, start with choosing the material itself — this article assumes that decision is already made and the question is who supplies it.
What an OEM Buyer Is Really Qualifying
The phrase "thermal interface material supplier" covers three different kinds of business, and they carry different risks. A material manufacturer formulates and compounds the material — the silicone or non-silicone base, the ceramic or boron nitride filler system, the cure chemistry. A converter buys finished material in roll form and die-cuts, laminates or adds adhesive backing to your drawing. A distributor resells and holds stock.
All three can appear on a quotation with the same logo and a similar price. The failure modes are not the same. A converter that runs out of a competitor's roll cannot change your formulation — but it can substitute an equivalent grade and never tell you. A distributor cannot control anything upstream of its own warehouse. A manufacturer can change a filler supplier and alter the thermal performance of every part you receive afterwards.
Some companies present as a thermal management material supplier and carry pads, foams, tapes and potting compounds side by side. That breadth helps on the programs where a thermal management stack needs more than one material family at once — a pad on the die side, a gap filler across the module, a foam seal on the enclosure — because qualifying three separate suppliers is real engineering time. It does not tell you which of those product lines the company compounds itself and which it buys in, so ask that line by line.
Applications pull the questions in different directions too, and a supplier that has never run them will not have the data. A die-cast LED luminaire puts outgassing and long-term color stability ahead of raw conductivity. A CPU, GPU or power electronics module built around an IGBT or a SiC device cares more about compression force, warpage and dielectric strength. Where the material sits between a die and a heat sink under high clamp load, the useful number is the one measured at that load, not at a nominal 10 psi.
This matters because thermal interface materials sit in the stack where almost nothing else can compensate. A 0.5 mm gap filler that pumps out of the bond line will raise junction temperatures on a power module even if the die attach and the cold plate are perfect. The material is cheap relative to the assembly and expensive when it fails, which is exactly the asymmetry that makes supplier selection worth an afternoon of work.
The eight checks are designed for that asymmetry. They also work as a pass/fail filter rather than a scoring exercise: a supplier that cannot answer check 4 or check 6 is not a lower-ranked supplier, it is a supplier you cannot audit later.
The 8-Point Checklist at a Glance
Use the table as a working supplier qualification checklist. The last column is the part most buyers skip: the answer that should stop the qualification rather than start a negotiation.
| # | What you are checking | Evidence that satisfies it | Stop signal |
|---|---|---|---|
| 1 | Certification scope | IATF 16949 / ISO 9001 / ISO 14001 certificate with scope, site address and validity dates | A group certificate, or a scope statement that does not name the product family you are buying |
| 2 | Thermal data | Test method, test pressure, bond line thickness and sample conditioning on the datasheet | A single W/m·K number with no method, or laser-flash data offered as interface resistance |
| 3 | Process capability | Cpk on thickness and hardness, control plan, last 12 months of SPC data | "We test every batch" with no numbers, or a Cpk below 1.33 on a critical characteristic |
| 4 | Lot traceability | CoA per lot with lot number, cure date, test results and a shelf-life statement | A CoA you cannot tie to the reel, box or bag in front of you |
| 5 | Compliance documents | RoHS, REACH SVHC, PFAS and market-specific declarations, each naming the part number | A generic statement that covers the company rather than the grade ordered |
| 6 | Conversion capability | Die-cutting tolerance, tooling ownership, first-article report against your drawing | Tolerance quoted as a range with no inspection method, or tooling you have to buy twice |
| 7 | Capacity and lead time | Stated line capacity, standard and expedited lead time, named second source for raw material | Lead time quoted in weeks with no ramp commitment, or a single-source filler system |
| 8 | Commercial terms | Incoterms, HS classification, country of origin, price validity period, NDA and IP terms | Duty and clearance "handled by the forwarder" with no landed-cost breakdown |
The table is the deliverable. Everything after it in this guide exists to help you read the answers you get back — and to tell the difference between an answer and a brochure.
1. Certifications: Scope, Site and Validity
A certificate answers a narrower question than most buyers think. It says that a named site runs a documented, externally audited management system for a defined scope of work. It does not say anything about the thermal performance of the material you are buying.
Read three fields before you file the PDF. Scope — does the scope statement cover thermal interface materials, or a related product family instead? Site — IATF 16949 certification, for example, is granted to a manufacturing location, not to a brand; a certificate held by a sister plant in another country does not transfer to the site that will run your order. IATF publishes the current rules for how sites are certified and audited. Validity — a certificate that expired last quarter is a finding, not a formality.
For a thermal materials supply chain, the useful document set is small:
| System | What it tells you | Where it does not reach |
|---|---|---|
| IATF 16949 | Automotive-grade process discipline: control plans, MSA, contingency planning | Nothing about a specific grade's thermal or mechanical properties |
| ISO 9001 | A functioning quality system | Minimum bar; almost every candidate holds one |
| ISO 14001 | Environmental management, including controlled substance handling | Not a product compliance declaration |
| QC 080000 | Hazardous-substance process management (an electronics-industry scheme) | Does not replace RoHS or REACH declarations |
| UL component recognition | Flammability and material ratings for specific compounds | Not a system certificate — it attaches to listed grades |
That document set overlaps with the compliance file you will build at check 5, and the certifications and compliance hub covers how each of these documents is read for thermal materials.
Ask for the certificate registry entry, not just the certificate. UL Yellow Cards and IATF certificates both have public lookup paths, and a buyer who checks one at random signals to the whole supplier base that the paperwork is read. That single habit changes how substitutions get handled downstream.
2. Thermal Data You Can Actually Compare
This is the check where most comparisons quietly break. Two suppliers quote 3 W/m·K and the numbers are not the same measurement.
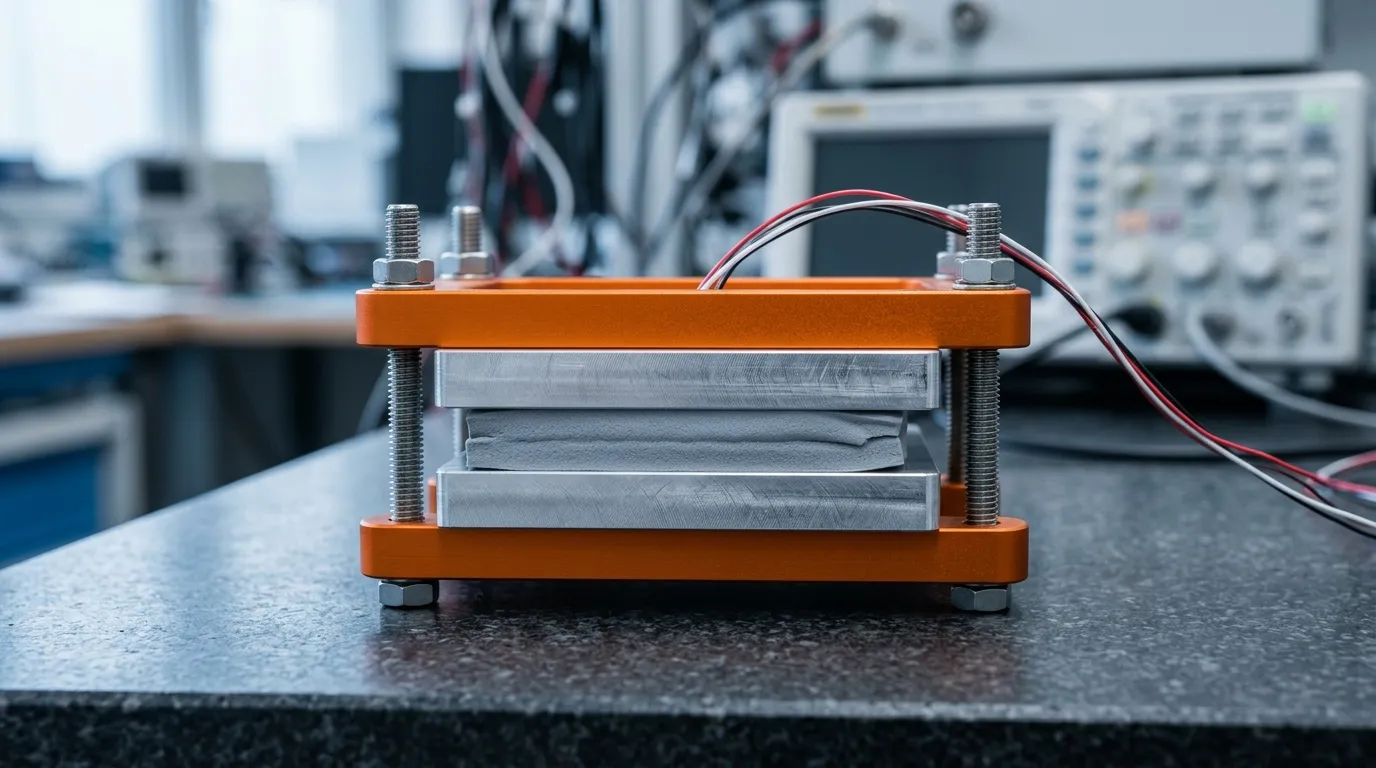
Thermal conductivity (k, in W/m·K) describes the material. Thermal resistance (in °C·cm²/W or °C·in²/W) describes the interface that the material forms under a specific pressure and bond line thickness — and the interface is what raises or lowers your junction temperature. The two quantities are related but not interchangeable, and the difference between resistance and impedance is worth settling before you compare anything.
Then check the method. The two methods you will see quoted most are bulk thermal conductivity by laser flash (ASTM E1461) and steady-state thermal transmission through a thin specimen (ASTM D5470). A laser-flash number is not a D5470 number. Laser flash measures how heat diffuses through a bulk specimen; D5470 measures the thermal impedance of a stack under a controlled load, which is much closer to how the material behaves between a die and a heat sink. A supplier who presents laser-flash values in a D5470 column, or who will not say which method produced a figure, has just told you something useful about its technical support.
Four data points belong on every datasheet you accept:
- Test method and revision — ASTM D5470, with the year, not just the standard number.
- Test pressure — 10 psi and 50 psi produce different numbers from the same pad. Without the pressure, a resistance figure is unfalsifiable.
- Bond line thickness or deflection — the thickness actually achieved under that pressure, not the nominal thickness of the pad.
- Conditioning — whether the sample was measured new, after thermal cycling, or after aging. Pump-out and dry-out are interface problems that show up after cycling, not on day one.
Phase change material (PCM) is the clearest illustration of why that last point matters. PCM is designed to flow at operating temperature, so a resistance figure measured cold describes an interface you will never actually run. Ask for the cycled number, and ask what the bond line does after a hundred cycles.
If your program puts the material on a bare die, an IGBT, a SiC module or a GPU with a warped package, add one more requirement: measured data at the gap you actually have, including the warpage range. Ask for the data in writing and treat "similar to" as an untested claim.
Where test reports come from matters too. A third-party report from a laboratory accredited under a mutual recognition arrangement such as ILAC carries more weight than an internal sheet, and the difference matters most for the compliance checks further down.
3. Process Capability: Cpk, SPC and Batch-to-Batch Consistency
A quality system certificate describes how a site is managed. Process capability describes what the site can actually produce, batch after batch, and it is the number that predicts whether month nine looks like month one. Thermal interface material quality is decided at this layer, not in the datasheet.
Ask for a capability study on the two characteristics that move your thermal result: thickness and hardness. Thickness drives the bond line; hardness drives how much the pad compresses at your assembly force. Both are usually quoted as a nominal with a tolerance, and both are frequently only marginally under statistical control in die-cut materials.
The specific request is a Cpk value per characteristic, against the tolerance on your drawing, computed from a meaningful sample over a defined period. A Cpk of 1.33 is the conventional floor for a significant characteristic in automotive work, and 1.67 is the conventional floor for one the customer classifies as safety-critical or key. Below the applicable floor, the process will produce out-of-spec material at a rate you will find during assembly. Be skeptical of a capability study run on three samples from one lot — that is a demonstration, not a capability.
Then ask the harder question: what happens when capability slips? The answer you want names a containment and corrective-action process — an 8D or an equivalent — with a commitment to notify you before non-conforming material ships. Suppliers who publish their own deviation process are describing a system; suppliers who promise to "always inform the customer" are describing an intention.
4. Lot Traceability: CoA, Labels and Shelf Life
Traceability is the check that feels bureaucratic until the day it is not. If a field failure traces back to interface material, your ability to quarantine the affected builds depends entirely on whether you can walk from a finished unit to a supplier lot number — and how fast.
Three things have to line up. The certificate of analysis for each lot should carry the lot number, the manufacturing or cure date, the test results for the characteristics you care about, and the specification limits they were compared against. The label on the reel, box or bag should carry that same lot number. The shipping document should reference it too. If those three disagree, traceability is a story rather than a system.
Shelf life is part of the same check. Silicone gap fillers, thermal greases and curable two-part gels change with age: viscosity drifts, cure behavior shifts, and shelf life is stated under specific storage conditions of temperature and humidity. Ask for the storage window, the recommended re-test interval, and whether the supplier will re-certify expired stock rather than quietly ship it.
One practical habit: sample the CoA against your own incoming inspection for the first three lots, then spot-check afterwards. A supplier whose CoA numbers are always perfectly centered on nominal, with no scatter, is reporting a specification rather than a measurement.
Automotive programs push traceability further — banked samples, certificates held for the life of the program, and a change process the customer can audit. If you are buying for that kind of program, automotive programs with lot-level traceability shows what the documentation set looks like from the supply side, which is a useful benchmark for what you should be asking your own candidates to produce.
5. Compliance Documents for Your Export Markets
Compliance is where a cheap quote becomes expensive, because a missing declaration stops a shipment at the border and a missing substance disclosure stops it in your customer's quality system.
Ask for declarations by part number, not by company. A folder of documents covering the manufacturer's whole portfolio tells you nothing about the grade you are buying. For most programs shipping into Europe and North America, the set looks like this:
- RoHS — restricted substances in electrical and electronic equipment. The European Commission's RoHS pages are the primary reference for scope and exemptions.
- REACH, including the SVHC candidate list — the REACH Regulation sets the duties, and two thresholds are worth keeping apart. A candidate-list substance present above 0.1% by weight in an article triggers your duty to inform your own customers; reporting to ECHA applies at that same 0.1% concentration once the amount of the substance contained in those articles exceeds one tonne per year.
- PFAS — per- and polyfluoroalkyl substances are under active regulatory attention in both the EU and the US, and they appear in some processing aids and release liners. EPA's PFAS pages are the US starting point.
- TSCA — for anything shipping into the United States, the EPA's TSCA program sets out the reporting and import obligations.
- California Proposition 65 — a separate state regime with its own warning requirement; the OEHHA list is the authoritative source for which substances trigger it.
- Full material declaration — an IEC 62474-style declaration saves your compliance team from re-asking for individual declarations later.
Two more questions belong in this section even though they are not strictly compliance. First, conflict minerals: if your product falls under a customer's 3TG reporting requirement, ask whether the supplier sources smelters audited under a recognized program such as the RBA's RMAP. Second, change notification: any substance change to a declared grade — including a new filler supplier or a processing-aid substitution — should trigger a written notice with a re-qualification window. That clause is usually the cheapest risk control in the entire supply agreement.
Substance lists and thresholds change on their own schedule, and they change by market. Confirm the current version of every declaration against the authority's own published list before you rely on it in a customer submission, and put a review date on your compliance file rather than treating it as closed.
If the material touches a flame-rating requirement, compare the flame rating the supplier lists against the specimen geometry your part actually is, because UL 94 V-0 and VTM-0 are applied to different specimen forms and cannot be swapped.
6. Conversion Capability: Die-Cutting, Tolerances and First Article
Most programs do not buy a roll. They buy a part: a die-cut pad with adhesive backing, a laminated stack, a pre-formed gasket, sometimes several materials married into one assembly step. So the supplier's converting capability is as load-bearing as its compounding capability.
Four things to settle in writing:
Tolerance and inspection method. A thickness tolerance of ±0.05 mm means little without the inspection method behind it. Ask what gauge, at what points across the part, and how many parts per lot. Tolerances that look tight but are never measured reappear as assembly problems.
Tooling ownership and transfer. Who owns the die, what does it cost to transfer, and how long is the die good for? If you are qualifying a second source, tooling that cannot move is a lock-in clause wearing a technical disguise. Data on thickness and compression behavior belongs in the same conversation — the thickness and compression data guide explains how those numbers interact with assembly force.
First article inspection. The first production run should produce a dimensional report against your drawing, not a sample in a box. A first-article report with measured values, not just pass/fail ticks, is what lets you approve a process rather than a part. Automotive buyers will recognize the shape of this as a PPAP-lite submission, and asking for it in a lower-stakes program is rarely resisted.
Interface with your assembly. Automated dispensing, robot placement, vacuum pick-up, reflow exposure — each constrains the material form and the liner. Tell the supplier how the part will be placed, then ask whether it has run that process before.
7. Capacity, Lead Time and Your Second Source
Lead time is a capacity statement wearing a date. A four-week quote and a twelve-week reality both come from the same supplier, and the difference is usually whether your volume lands on a line that is already full.
Ask three questions. What is the line capacity for this product family, expressed in square meters or parts per month? What is the committed lead time at your forecast volume, and what is the expedited path when a build slips? What raw materials have a single source upstream, and what is the supplier's plan if that source fails?
That third question is where a real answer separates suppliers. Filler systems, release liners, adhesives and carrier films often have one qualified source. A supplier that knows which one of its inputs is single-sourced, and can name a qualified alternative or a buffer stock policy, has done the contingency planning that an IATF or ISO 9001 system requires on paper.
Second sourcing deserves its own decision, separate from supplier selection. Finding a second source for a thermal interface material is not the same task as choosing the first one. Two qualified suppliers with different upstream supply chains reduce interruption risk; two suppliers buying from the same compounder do not. The mechanics of a changeover are set out in the drop-in replacement guide, and the short version is that a second source counts as real once it has been through check 2 and check 3 with your own parts.
8. Commercial Terms: Incoterms, HS Codes and Landed Cost
This is the section competitors based in North America and Europe do not write, and it is where a large share of real cost sits. The largest lever is usually the material form rather than the unit price: one EV battery program we worked on cut the bill of materials by 35% when pre-cut pads were replaced with a dispensed gap filler, which is documented in that battery pack thermal case study.
Start with the Incoterm. FOB, CIF, DDP and EXW move cost, risk and customs responsibility between you and the supplier, and they are not interchangeable labels on a quote. The ICC's Incoterms rules pages define the current set; if a quotation does not name an Incoterm, or names one from a superseded edition, the quotation is not comparable to the others beside it.
Then classification and origin. Thermal interface materials rarely arrive under a single obvious tariff line — depending on the form and the substrate, a die-cut pad, a tube of grease and a potted module assembly can classify differently. Your broker will ask for a description and a suggested code, and the supplier should provide one. The United States' Harmonized Tariff Schedule is the reference for US imports; the same exercise in the EU uses the combined nomenclature. Country of origin must be documented too, because it drives both duty and preferential treatment. The search term buyers actually use — the HS code for a thermal interface material — usually resolves to a classification question rather than a fixed number, and the supplier who can explain that clearly is worth the conversation.
Finally, price validity and the commercial wrapper. Ask for the validity period and what resets it, typically a raw material index. Agree the NDA before sharing drawings, and settle the IP position on custom formulations: who owns a compound developed for your application, and on what conditions may it be sold to a competitor. Buyers who skip this step usually discover it matters once a successful program makes both questions relevant.
From the supplier's side of this, three things change when the manufacturer is in Asia, and they are worth pricing in before the RFQ goes out. Origin paperwork has to be agreed up front, because a certificate of origin and the declaration on the commercial invoice must say the same thing — a mismatch is resolved at the border, not in a meeting. Production geography matters more than the headline lead time: a supplier whose manufacturing is spread across more than one country, as ours is across Dongguan, Kunshan, Taiwan and Vietnam, can shift volume between sites when one of them is disrupted, and that is a different kind of insurance from qualifying a second supplier. Overlap in working hours decides how painful the relationship is day to day; a clear response commitment — being told within two hours what happened and having an engineer on site within four is the standard we hold ourselves to — removes most of the friction buyers expect from an offshore supply chain.
How to Qualify a Thermal Interface Material Supplier in 30 Days
The eight checks are a document set, a set of questions and one visit. Here is a sequence that fits a normal project calendar.
Sequence matters more than depth. Most disqualifications are visible by the end of week 2 — before anyone has quoted a price.
Week 1 — issue, don't interview. Send the checklist as part of the RFQ, with the Incoterm, the annual volume and the drawing. Suppliers who answer in a structured way in week 1 are showing you their process. Suppliers who reply with a brochure have answered check 1 through check 8 in one move.
Week 2 — desk review. Score each response against the table above. Request the raw materials for the three checks that need documents: a CoA for a recent lot, a capability study, and the compliance declarations for the exact part number. This is also when you compare the thermal data properly — method, pressure, bond line and conditioning.
Week 3 — samples, on purpose. Build a small design-of-experiments style evaluation rather than a single "sample looks fine" build: two gap sizes, two assembly forces, and a thermal-cycling leg. Run your own electrical or junction-temperature measurement if you have it; if you do not, at least record the assembly outcome and inspect the material after cycling. In one of our own control-board projects, a MOSFET-to-enclosure interface change took the peak junction temperature down by 18 °C and moved assembly yield from 92% to 98.5%. Results of that shape are the reason the sample leg gets its own week rather than an afternoon.
Week 4 — audit and decide. A one-day site visit should cover incoming inspection, compounding, the die-cutting line, the test bench and the quarantine area for non-conforming material. Ask to see a recent 8D or corrective-action report, with the customer names removed. Then decide: approve, approve with conditions, or stop.
Approval with conditions is the normal outcome. Write the conditions into the supplier agreement — a follow-up capability study within 90 days, a first-article report on the first production lot, a re-qualification trigger on any formulation change — and the qualification stays useful instead of becoming a one-time ceremony. Where the interface sits outdoors or in an enclosure with wide temperature swings, add an environmental leg to the same sequence; how a second-source TIM is qualified for 5G hardware is a reasonable pattern to copy.
Red Flags That Should Stop the Qualification
Most of these appear in writing, which is why they are worth a list.
| Red flag | What it usually means |
|---|---|
| W/m·K quoted with no test method, or laser-flash data offered as interface resistance | The vendor is repeating marketing numbers and cannot support a design decision |
| Thermal data at a single pressure, with no bond line thickness | The number is not comparable to your application; expect a surprise at assembly |
| "We test every batch" but no Cpk, no control plan, no sample size | Quality is asserted rather than measured |
| CoA that does not match the label on the box | Traceability will not survive a field failure investigation |
| Compliance declarations covering the company, not the part number | The grade you ordered may never have been assessed |
| Lead time given as a single number, with no capacity or expedite answer | Capacity is being managed by promise rather than planning |
| Tooling owned by the supplier with no transfer clause | Your second source is not actually available |
| Quote with no Incoterm, or a superseded one | Landed cost is unknown and the comparison is invalid |
Two or three of these in one response is not a negotiation position. It is a signal to spend the week on the next candidate instead.
FAQ
What does TIM stand for in engineering, and is a TIM supplier different from a thermal pad supplier? TIM stands for thermal interface material — the family that includes thermal pads, gap fillers and thermal gels, thermal grease or paste, phase change materials, and graphite or metal-based interfaces. A thermal pad supplier is a TIM supplier whose range is limited to pads, which is common among thermal pad manufacturers serving consumer electronics. The distinction matters at check 6 and check 7: a broader form factor range gives you more options for a gap that changes during the program, and fewer suppliers to qualify separately. The thermal interface material guides cover the format-by-format comparison if you need to map the family first.
Is TIM the same as thermal paste? No. Thermal paste, or thermal grease, is one TIM format among several. It performs well at very thin bond lines and is usually applied by dispensing, which constrains assembly. Pads, gap fillers and phase change materials cover larger and more variable gaps. The selection question is a gap-and-pressure question, and it is answered in the material selection guide.
How long does qualifying a second thermal interface material supplier take? For a standard grade with an existing drawing, four to six weeks is realistic: two weeks of documentation and data review, two weeks of sample builds, and one site visit. A custom formulation adds four to six weeks for compounding and third-party testing, and automotive programs add the PPAP cycle on top. The schedule is usually set by your own sample builds rather than by the supplier's paperwork, so book assembly time before you start asking for samples.
Using This Checklist on Your Next RFQ
The eight checks are designed to be pasted into a request for quotation. Send the table, ask for the evidence column, and set a date. The answers you receive in the first week will sort the candidate list faster than any scoring model, and the two or three suppliers who answer all eight properly are the ones worth a site visit.
For a starting point on what a complete answer looks like, the thermal interface material range shows the form factors involved on the manufacturing side — pads, gap fillers, greases, phase change materials and combination parts — which is useful context when you compare a specialist converter against a material manufacturer.
Start with check 2 and check 3. Thermal data you can compare, and a process capability number you can audit, will tell you more about a supplier than the price column ever will.
If those are the two answers you cannot get, the ZIITEK thermal engineering team will take the same eight checks against your drawing and tell you which of them we can answer today and which we cannot — no quotation attached, and no obligation to run an RFQ afterwards.
Two disclosures. This guide is written by a thermal interface material manufacturer, so the sections on supplier capability describe the side of the table we sit on; read them knowing that. The images are illustrative industrial scenes, not photographs of any specific customer's or supplier's facility.